Fabrication and assembly, under one roof
Value-Added Mechanical Assembling for Custom Enclosures
Enclosuremfg combines sheet metal fabrication with mechanical assembly on the same production floor. Receive finished units ready to mount into equipment or field installations—with no additional mechanical work at your facility.
- 7 dedicated machinesFor clinching and tapping
- 10–300 unitsTypical production volumes
- 3 working daysDFM summary and fixed price
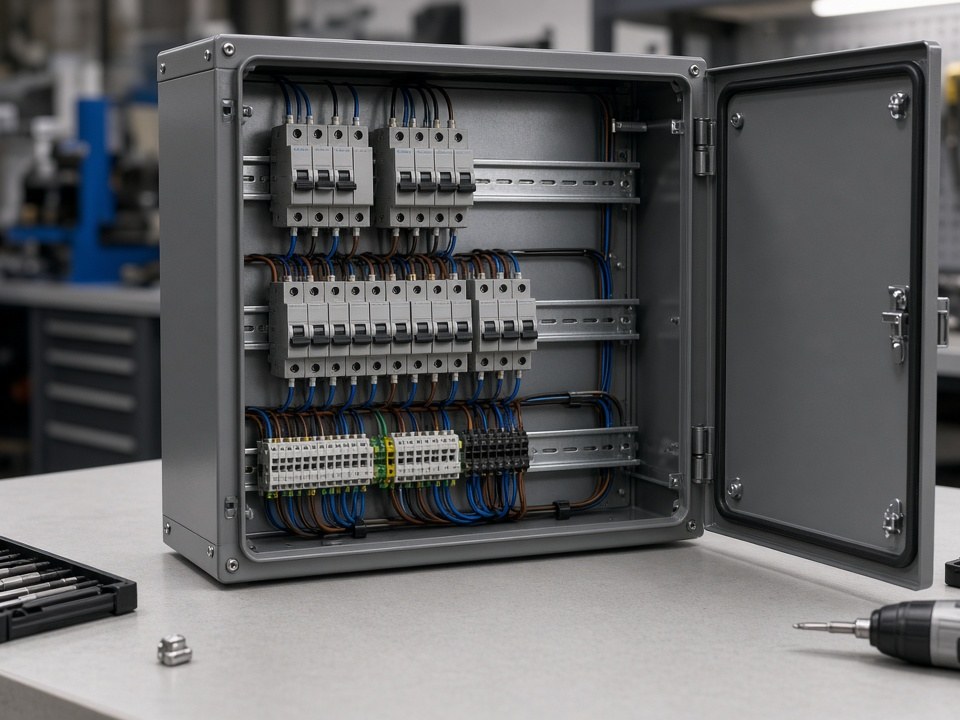
Ready for installation
Hardware insertion, access components, grounding points, and internal rail systems can be assembled and documented before shipment.
A connected production sequence
Assembly steps after fabrication
After laser cutting, bending, and welding, parts move to dedicated hardware integration stations. Fixed fixtures help maintain alignment across batches and replace disconnected vendor steps that can cause schedule gaps and tolerance stack-up.
-
01
Fabricate
Laser cut, bend, and weld enclosure components.
-
02
Insert and tap
Install fastening hardware and create required threads.
-
03
Pre-fit access hardware
Align hinges and locks, secure them to controlled torque, and seat gaskets.
-
04
Verify and document
Check assembly details and prepare hardware and torque records for incoming inspection.
In-house equipment and checks
Hardware integration built for repeatability
Seven dedicated machines support clinch fastening and tapping. Three automatic clinchers install PEM nuts, studs, and standoffs at rates suited to 500-unit runs without backlog.
Automatic clinching
Three automatic clinchers efficiently install PEM nuts, studs, and standoffs.
Servo tapping
Two servo tappers create clean threads in pre-punched holes.
Drill-tapping
Two drill-tappers handle mixed material stacks. Insertion points receive 100% torque sampling before the next station.
Fit, finish, and functional checks
Access hardware and grounding, pre-assembled
Hinges and quarter-turn locks are positioned with locating pins and secured under controlled torque. Gaskets are seated in the same pass to help prevent later rework. Assemblies leave the line with doors that open and close to specification.
This pre-fit service supports NEMA 4 and IP66 configurations common in energy storage and telecom cabinets.
Grounding studs and rail systems
- Grounding studs installed with calibrated torque drivers and marked for inspection.
- Verification label for each stud, showing torque value and operator ID.
- DIN rails, mounting plates, and cable management channels assembled using the same fixture set.
- Ready-to-use grounding points eliminate the need for electricians to drill or tap on-site.
Turnkey delivery scope
Finished units, with assembly records
Completed units ship with mechanical hardware installed and documented, ready to mount into equipment or field installations.
4–6 hours
of assembly labor per unit customers report eliminating at their own facilities.
Typical package contents
- Enclosure body and doors
- Side panels and internal rails
- Grounding points
- Lock hardware and hinges
Documentation lists part numbers and torque records to support incoming quality checks.
For equipment builders
One assembly partner across demanding applications
Typical volumes run from 10 to 300 units, with repeat annual schedules.
Industrial machinery
Operator consoles and machine guards that require frequent access hardware.
Energy storage and inverters
Cabinets with pre-installed rails and grounding ready for power electronics.
Telecom integration
Weatherproof boxes with locks and hinges aligned for field crews.
Request current lead time and pricing
Share your drawings and hardware specifications
Provide 3D files or 2D drawings along with hardware specifications. Our engineering team returns a DFM summary and fixed assembly price within three working days.
Facility visits can be arranged at Building 4, Kuiqing Road, Qingxi Town, Dongguan City, Guangdong Province to review fixture setups and finished samples.
info@enclosuremfg.com